From Raw Material to Pure Strength

State-of-the-art induction melting, continuous billet casting, precision rolling, and thermo-mechanical treatment.
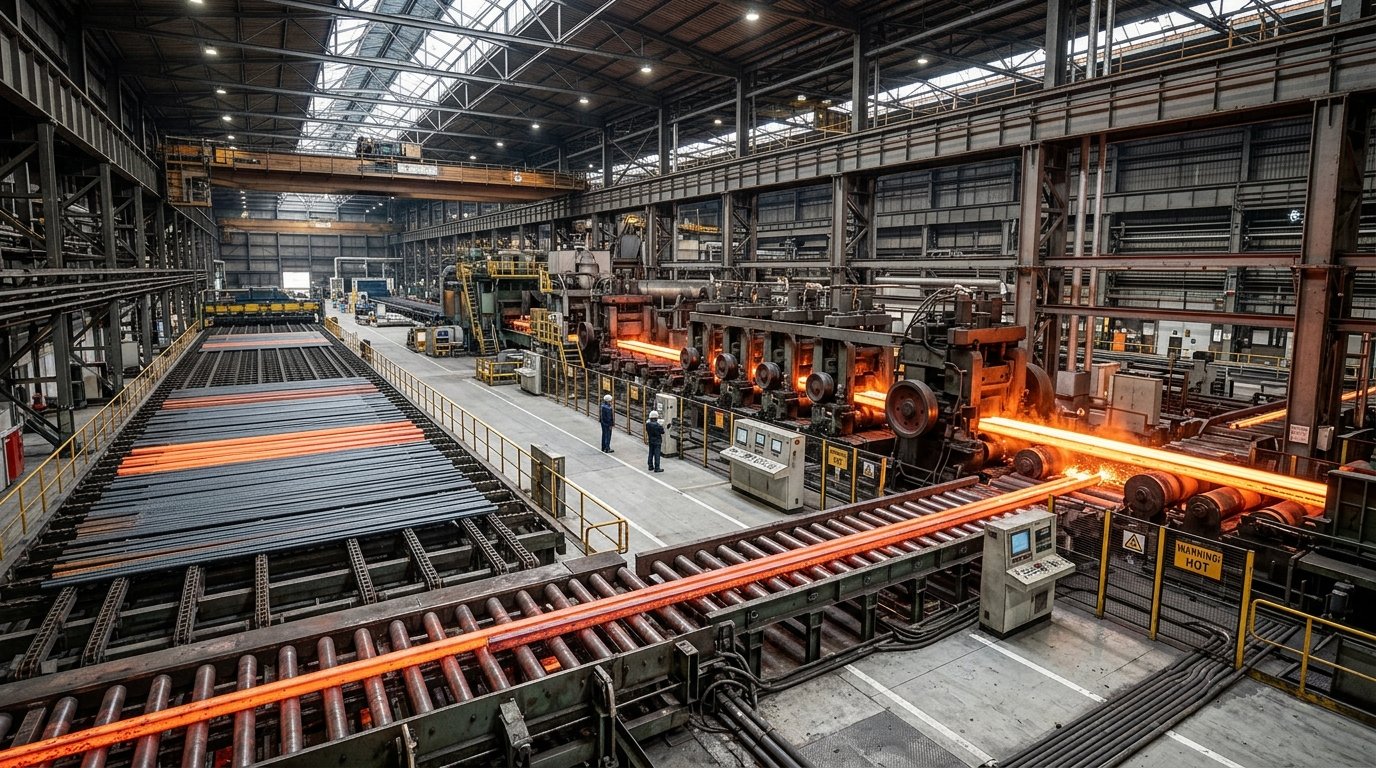
Metallurgical Precision At Scale

The manufacturing philosophy of Avinashi Steel unites pure metallurgical raw materials with high-speed automated rolling mills. Rather than relying on cold twisting or surface hardening alone, our integrated process employs Thermo-Mechanical Treatment (TMT)—a thermal quenching and self-tempering process that reorganizes the crystalline steel structure from the molecular level.

[ADD OFFICIAL AVINASHI MANUFACTURING FACILITY OVERVIEW & CAPACITY MILESTONES HERE. To be updated with confirmed plant acreage, furnace specifications, mill speed, and continuous casting dimensions upon official client submission.]

"जब नींव हो अविनाशी तो इमारत बने विश्वासी"

Continuous Rolling Stand

THE 8-STEP MANUFACTURING SEQUENCE

A meticulously calibrated metallurgical pipeline transforming prime inputs into defect-free structural rebars.

01

Raw Material Inspection

Incoming sponge iron, high-grade scrap, and virgin ferro-alloys are assayed in our lab to ensure strict sulphur and phosphorus suppression before charging.

02

Induction Furnace Melting

Molten steel is refined at 1600°C in high-capacity medium-frequency induction furnaces with secondary ladle refining for exact alloying homogeneity.

03

Continuous Billet Casting (CCM)

Liquid steel is cast through curved mold continuous casting machines into solid, uniform, defect-free square steel billets.

04

Hot Reheating & Continuous Rolling

Billets are soaked in reheating furnaces and passed through automated roughing, intermediate, and finishing mill stands with CNC tungsten carbide rolls.

05

Thermo-Mechanical Quenching

Red-hot rebars exiting the final stand enter a proprietary water-quenching chamber. The surface is rapidly cooled to form an outer martensitic ring.

06

Self-Tempering & Core Cooling

On the cooling bed, heat flows from the hot austenitic core to temper the martensite surface, while the inner core transforms into ductile ferrite-pearlite.

07

Cold Shearing & Bundling

Automated cooling beds transfer straightened bars to flying shear cutters calibrated to standard 12-meter lengths, ready for mechanical bundling.

08

QR Barcode Tagging & Dispatch

Every bundle receives tamper-evident metallic tags stamped with heat number, nominal diameter, and QR authentication before trailer loading.
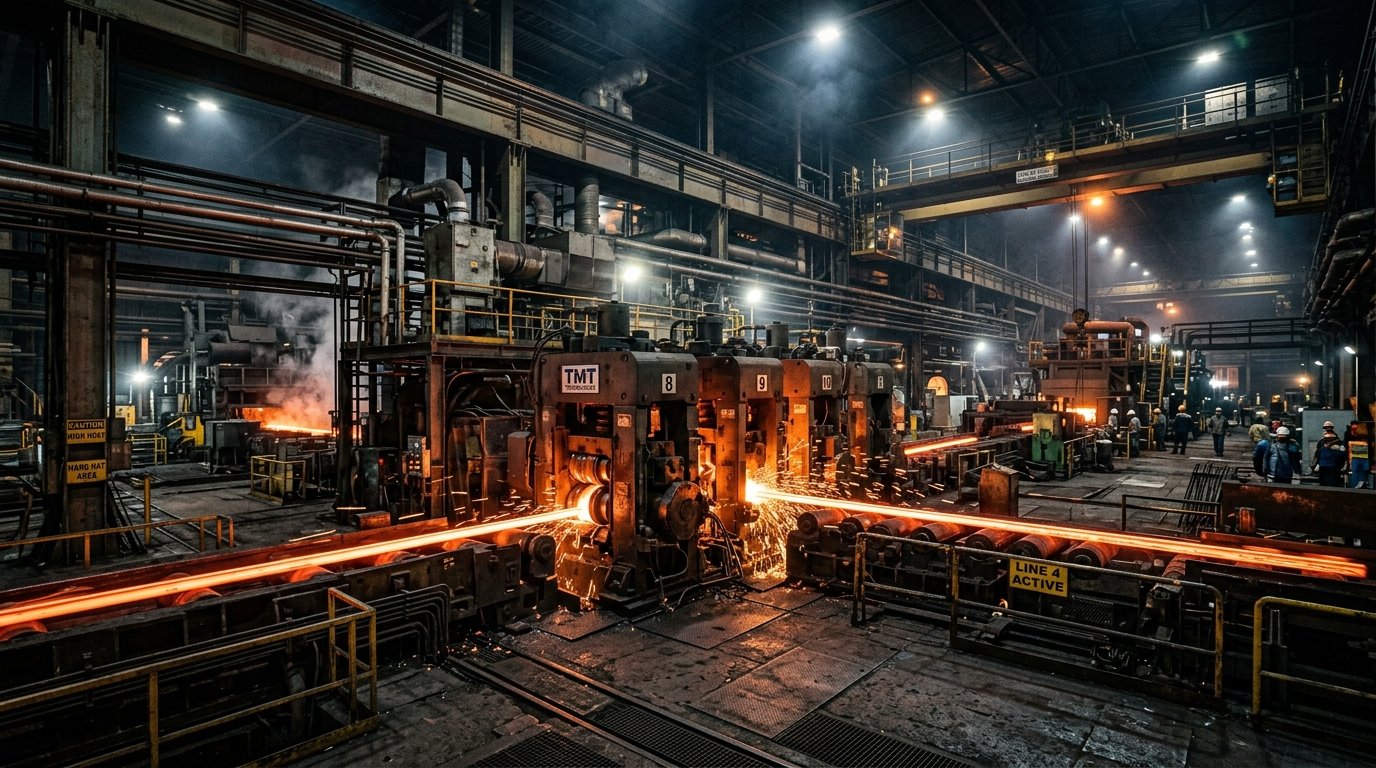
Avinashi Rolling Mill Technology

The Science Behind The Concentric Ring

The signature strength of Avinashi TMT rebars lies in its concentric dual-phase microstructure:

  • 1
    Outer Layer: Tempered Martensite Provides high surface hardness, abrasion resistance, and high proof stress to handle compressive structural loads.
  • 2
    Inner Core: Ferrite-Pearlite Maintains exceptional ductility and energy absorption capacity, allowing the steel to flex during earthquakes without snapping.

Schedule A Plant Inspection

Institutional buyers, EPC contractors and consultants are welcome to review our manufacturing standards.
Request Plant Visit